Understand the different questions behind DFM and DFT
A DFM review asks whether the chosen fabrication and assembly processes can consistently produce the design. Trace and space, drilling, footprint geometry, solder mask, component access and panel handling belong here. DFT asks how the finished assembly will be verified: what is measured, where the probes connect, how firmware is loaded and which result supports an acceptance decision.
The concerns interact. A test pad beneath a large connector may be inaccessible after assembly. An edge component can interfere with panel separation or fixture support. Discuss the same revision across teams and resolve these specific conflicts rather than relying on the length of a checklist.
Translate the selected process into CAD rules
Match stack-up, material, copper, trace spacing, drill and annular-ring rules to the actual manufacturing option. A fine feature may need a different process or cost. Electrical safety spacing has separate requirements; the factory’s minimum capability does not establish a safe product layout.
Review schematic ERC and PCB DRC results, documenting justified exceptions. A clean report does not establish mechanical fit or correct part selection. Inspect the profile, cutouts, drill types and layer order in an independent CAM view. Distinguish plated and non-plated holes and identify the actual board outline clearly. Ambiguous fabrication instructions should be resolved before the release package reaches the supplier.
Review footprints, polarity and physical assembly access
Verify library components against manufacturer drawings: pads, numbering, dimensions and land patterns. Pin one must agree across legend, assembly drawing and placement data. Diodes, LEDs, polarized capacitors and connectors need orientation marks that remain understandable after placement. Hidden marks provide little help.
Allow space for soldering, inspection and repair. A small part beside a tall component, an inaccessible joint or a component beneath a screw head deserves attention during layout. Agree transport edges, fiducials and panel separation with the assembler. Avoid using one memorized clearance for every product: the selected process and the mechanical design determine the practical constraint.
- Do manufacturer part number, footprint and placement data describe the same component?
- Can rotation and pin-one convention be confirmed during first-article review?
- Are mask openings, narrow mask features and legend over pads checked?
- Can connector latches, screws and enclosure features still be accessed after assembly?
Derive test points from the measurement plan
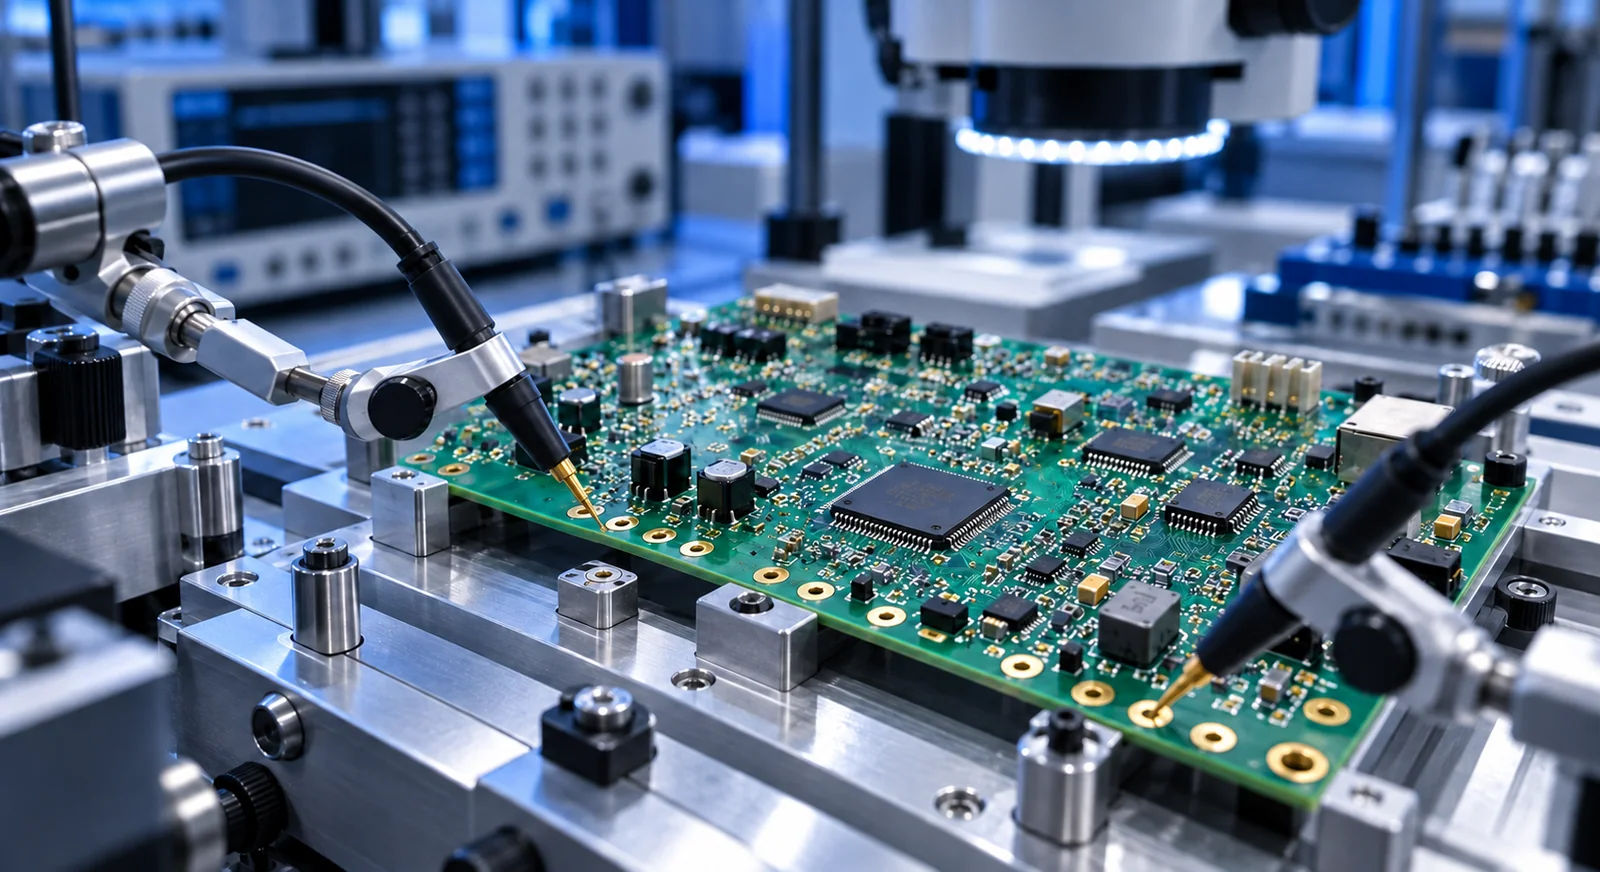
Testability requires more than adding exposed copper to unused space. Identify required measurements for rails, grounds, reset, programming and critical I/O first. Evaluate net access against the intended test method. A pad or long branch added to a high-speed or sensitive analog signal can affect circuit behavior, so the electrical design must be reviewed alongside the access requirement.
Agree pad size, spacing, edge clearance and access side with the fixture team. A masked pad or hidden via is unusable regardless of its testpoint property. CAD rules and reports help review access. Match net names, references, coordinates and board side to the fixture documentation.
| Area | Example access | Information needed at release |
|---|---|---|
| Power | Input, regulator outputs and ground | Voltage limits and safe power-up conditions |
| Programming | Interface, reset and reference | Pinout and firmware package revision |
| Analog | Critical signal and suitable reference | Stimulus, tolerance and measurement conditions |
| Output | Load connection and feedback | Load type, duration and acceptance limit |
Try the programming and operator workflow
The development cable used at a bench may not suit production. If a programming connector is removed from the final product, solve probe access, board support and connection order during design. Consider mechanical references that discourage inserting the board incorrectly. Review whether externally applied power or signals could back-power another connected circuit while the fixture is operating.
At the fixture trial, assess insertion time, repeatable contact, orientation marks and safe removal. Current limits, software selection and failed-unit segregation must be clear. Resolve any test that cannot be performed by changing access, fixture or method, then approve the revised coverage.
Release one consistent revision with measurable criteria
Schematic, fabrication data, drills, BOM, placement file, assembly drawing and firmware must belong to the same released revision. Use explicit revisions and dates instead of filenames such as “final2”. Identify DNP positions, approved alternatives, special assembly notes and the software package used during testing. A release manifest helps the receiver distinguish intentional variants from missing information.
A second reviewer can find inconsistencies the designer overlooks. Record pilot-build assembly and test times, false calls and repair causes. Feed results into controlled schematic, layout and test-document changes. This creates a feedback loop and gives subsequent production runs a reason for each changed rule or test.
Frequently asked questions
Does a clean DRC report mean DFM is complete?
No. DRC checks the rules that were defined. Wrong footprints, assembly access, mechanical fit, panel handling and incomplete release instructions still need separate review.
Is there one correct test-pad diameter?
No universal diameter applies. Probe type, fixture tolerance, access direction, available space and process requirements matter. Agree dimensions and spacing with the fixture team while the layout can still change.
Can I add test points after completing the PCB?
It is possible, but late changes can introduce access and signal-integrity problems. Defining coverage during schematic and placement work reduces last-minute routing changes and fixture restrictions.
Conclusion and next step
A production-ready board needs repeatable assembly, usable measurement access and explicit limits. Align DFM and DFT checklists with supplier capability, test methods and pilot feedback. A consistent revision package and exercised test steps support a controlled manufacturing release.
Request a PCB Manufacturability and Testability Review
Technical references
The following manufacturer and technical organization documents provide further detail. Use the selected component’s current data sheet for product-specific limits.