Start with failure modes, then select the methods
List what can go wrong before choosing the test station. A missing resistor, a reversed diode, a bridge beneath a BGA, incorrect firmware and a power rail that collapses under load need different checks. Assign each risk a method, an acceptance limit and a recorded result.
The table describes typical emphasis, not guaranteed coverage. Package geometry, camera access, probe access, equipment capability and program development determine what a station can detect. Review this map after pilot builds. An unexpected failure may expose a coverage gap, a design problem or an assembly process needing closer control.
| Method | Primary question | What it cannot establish alone |
|---|---|---|
| AOI | Are visible assembly features correct? | Firmware behavior and operation under load |
| X-ray / AXI | Are hidden solder structures acceptable? | All electrical product functions |
| ICT | Do accessible nodes meet electrical expectations? | Every operating scenario |
| Functional test | Does the board respond correctly to defined stimuli? | The physical quality of every joint |
AOI provides early feedback on visible assembly
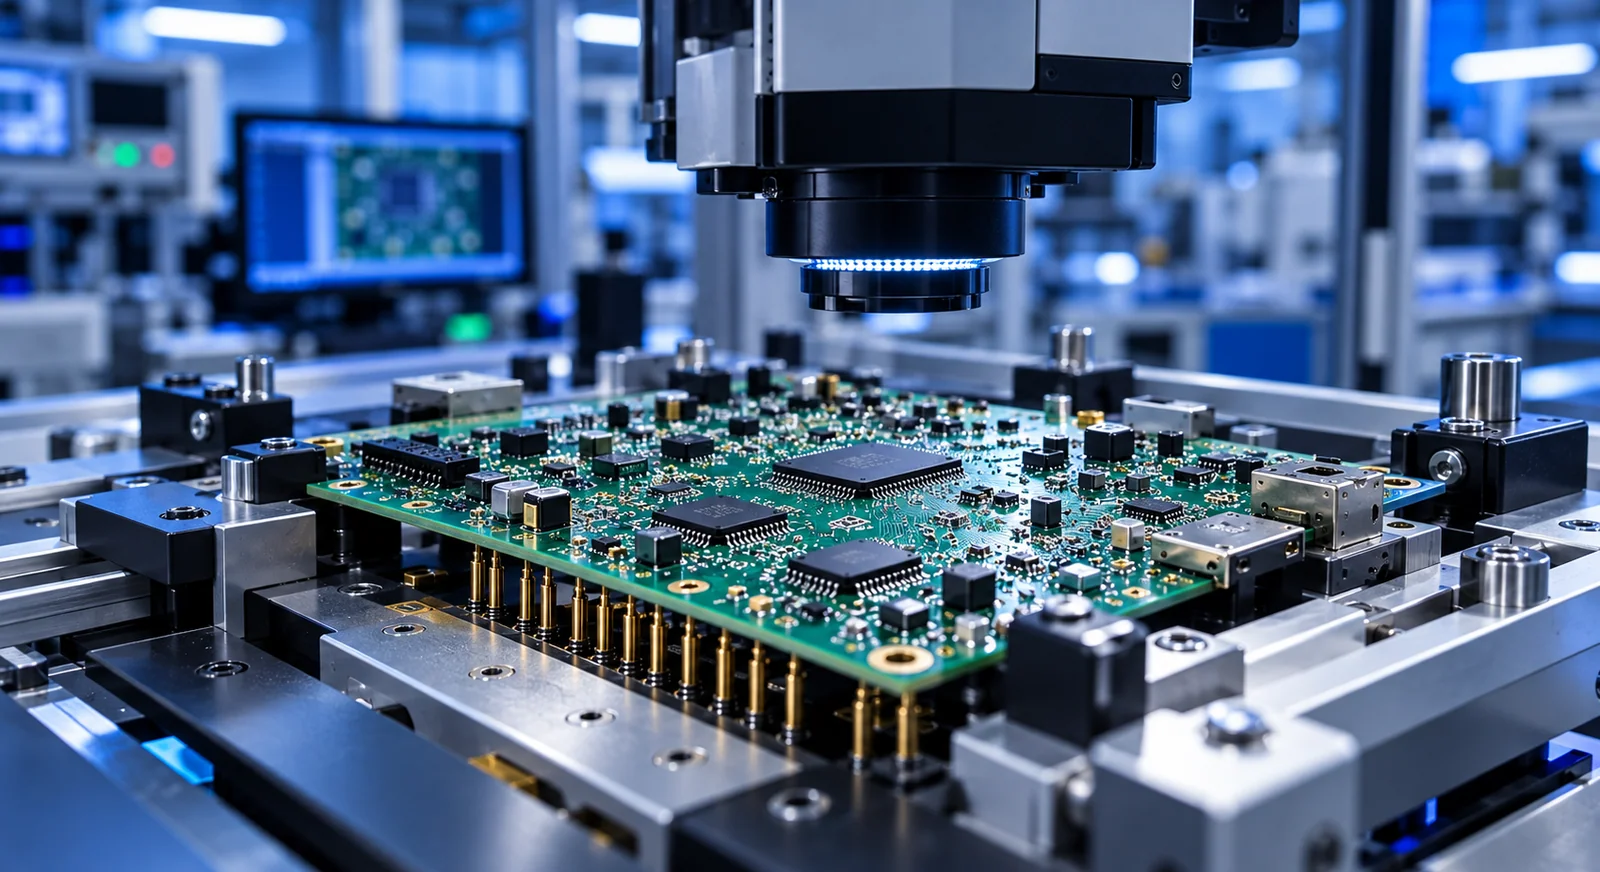
Automated optical inspection uses cameras and a programmed inspection model to assess component presence, position, orientation and accessible solder features. Two-dimensional and three-dimensional systems offer different measurement capabilities. With a suitable program, missing or displaced components, some polarity errors and visible solder bridges can be identified close to the assembly process.
A camera cannot reliably distinguish every electrically different part with the same marking. Obscured joints and internally damaged devices require other evidence. Validate the program on the first build, review false calls and retain approved revisions. Overriding alarms without investigating their cause weakens the process.
X-ray examines connections that cameras cannot see
BGA balls and some bottom-terminated package connections are outside normal optical access. X-ray inspection can examine solder distribution, bridges and void structures in these regions. A two-dimensional image may contain overlapping features from both sides of a board. Appropriate three-dimensional or CT techniques can help separate structures for a more useful interpretation.
An image needs an acceptance criterion appropriate to the package and product. Treating every void equally or applying one percentage to all connections is unsound. Agree critical regions, image settings and follow-up analysis before production. The result describes the inspected structure; it does not establish correct firmware or loaded-output operation.
ICT looks for electrical assembly faults at circuit nodes
In-circuit testing accesses selected circuit nodes through a fixture or suitable probes. Appropriate techniques can detect shorts, opens, some wrong component values and orientation faults. Parallel circuit paths can influence a measurement, so an in-circuit resistance check is not always equivalent to placing a meter across an isolated resistor. Test development must account for the surrounding circuit.
A net without probe access may require extra engineering or reduced coverage. Provide the schematic, netlist, BOM and critical-net priorities together. ICT can narrow a fault location, while firmware and loaded outputs need separate checks. Plan ICT and functional testing together to expose these coverage boundaries.
Functional testing turns product behavior into measurements
A functional station powers the board under defined conditions, applies stimuli and measures responses. A power LED is rarely a sufficient acceptance criterion. Supply range, standby current, relay output, analog accuracy and communication responses can each become a separate step. Specify stimulus, settling time, unit and lower and upper limits so that different operators obtain comparable decisions.
For an illustrative 24 V sensor board, a sequence might use current-limited power-up, a 3.3 V rail check, a known analog input and a communication command that reads the result. An output is then exercised with a representative load. These are example steps, not universal limits: the product requirements determine values and conditions. Track the test program revision alongside the device firmware revision.
Control the sequence, retests and recorded evidence
Assembly review and appropriate unpowered short checks can precede controlled power-up and functional measurements. Adapt the sequence to product risks. Decide which checks run again after repair; repeating only the last failed step may miss a change introduced during rework.
Measurements tied to a serial number or batch allow investigation of drifting rails, worn contacts or incorrect software selection. A reference board and known faulty samples help check station behavior. Record calibration, fixture maintenance and intermittent failures too: a changing station can otherwise look like a changing product.
- Record the critical failure mode, detection method and remaining coverage gap.
- Evaluate acceptance limits against requirements and measurement uncertainty.
- Define segregation, repair and retest rules for failed assemblies.
- Save board, firmware, fixture and test-program revisions with the result.
Frequently asked questions
Does a board that passes AOI still need functional testing?
Its required behavior needs separate verification. AOI evaluates visible assembly features, while loaded outputs, firmware, communication and measurement accuracy require suitable operating checks.
Does every PCB assembly require X-ray inspection?
The scope depends on its packages and product risk. Hidden solder connections deserve explicit review. Full inspection, sampling or inspection of selected regions should be agreed for the project.
Can a board pass functional testing with a solder problem?
Yes. A weak connection may make contact during the test, or a defect may lie outside the exercised scenarios. Imaging, electrical checks and functional testing provide different evidence and should be planned accordingly.
Conclusion and next step
A useful test plan connects risks to acceptance evidence. AOI, X-ray, ICT and functional testing are complementary. Discuss package construction, probe access, measurable limits and traceable results together to focus failure investigation and expose recurring process problems.
Discuss the Manufacturing and Test Scope for Your Board
Technical references
The following manufacturer and technical organization documents provide further detail. Use the selected component’s current data sheet for product-specific limits.